COST ANALYSIS & RISK GUIDE
An operator-level breakdown of what actually happens — mechanically and operationally — when a round baler PTO shaft is the wrong series, wrong length, or wrong spline for the baler and tractor it connects.
The round baler PTO shaft is rarely the most expensive component on the machine, which is precisely why operators sometimes replace it with whatever is available locally, the cheapest option from a generic supplier, or a second-hand shaft pulled from a different baler model. The shaft itself may install without obvious difficulty — it connects at both ends, the guard clips on, and the baler runs. What the operator cannot see during the first hours of use is the cascade of mechanical stresses building in the driveline: a Series 4 shaft running peak loads designed for a Series 6, a collapsed length that bottoms out at full steering lock, a spline mismatch that creates fretting wear at the yoke bore, or an operating angle that the U-joint was not rated to handle continuously. These are the hidden costs — the ones that show up weeks later as a gearbox failure during the critical second cut, or as a collapsed tube in the middle of a field with no spare on hand.
This guide quantifies the real downstream consequences of using an incorrect pto shaft for round baler applications, and explains exactly which specification errors produce which failure modes — so operators can make an informed decision before the season opens rather than an expensive repair decision after it has already failed.
Wrong Shaft Series: The Torque Mismatch That Compounds Over Time
The shaft series — 4, 6, or 8 — is not a brand classification. It defines the outer tube diameter, wall thickness, U-joint cross body size, and peak torque capacity of the complete assembly. A Series 4 shaft is rated to approximately 1,200 Nm peak torque. A Series 6 reaches around 2,100 Nm. The difference matters because a modern high-output round baler operating at 1000 RPM in heavy first-cut grass or corn stover generates instantaneous peak loads that regularly exceed 1,500 Nm during blockage events and slug feeding. Fitting a Series 4 shaft to a baler that specifies Series 6 — because the Series 4 was available quickly or was significantly less expensive — places the shaft in a cycle of repeated sub-failure overloads that it was not designed to absorb.
The damage does not present as a sudden catastrophic fracture in most cases. The undersized U-joint cross develops micro-cracks at the trunnion base — the highest stress point during each overload cycle — after which every subsequent rotation propagates those cracks a fraction further. The shaft continues to function and appears visually intact until the crack reaches a critical length, at which point the cross fractures under a load that would have been unremarkable on a correctly specified component. In a John Deere 469 or 569 baler context, where the operating environment demands continuous Series 6 capacity, a Series 4 round baler PTO shaft will typically fail within one to two seasons regardless of brand, grease interval, or slip clutch setting.
Wrong Shaft Length: Two Failure Paths from the Same Error
Shaft Too Short — Tube Collapse at Headland
A shaft that is too short in its collapsed position hits its minimum travel limit during tight headland turns. When the inner and outer tubes bottom out — the inner tube contacting the outer tube’s closed end — the shaft cannot compress further. Instead, the force that would compress the shaft is transferred directly into the yoke connections, pushing the baler hitch away from the tractor or bending the implement tongue. Operators often interpret this as a tractor steering problem or a hitch height issue and compensate by adjusting the drawbar rather than addressing the shaft length. Over time the repeated impact at the collapsed limit damages the tube end and the yoke bore, and the next observable symptom is a shaft that is loose and rattling even when correctly extended.
Shaft Too Long — Inadequate Tube Overlap
A shaft that is too long in its extended position draws the telescoping tubes apart beyond the minimum safe overlap length — typically defined as one-third of the inner tube working length in contact with the outer tube. Below this overlap, the torque transmission area between the tube profiles is insufficient to resist the torsional load without shear deflection. In practice, the tube profiles twist slightly against each other under load, generating fretting wear at the spline contact surfaces that is invisible from outside the guard. The operator notices nothing until the tubes have worn to the point where play develops — and at that stage the shaft must be replaced rather than serviced.
Wrong Spline Configuration: The Misfit That Wears Invisibly
Spline mismatches are common when a shaft is sourced without verifying the tractor PTO output configuration against the shaft yoke specification. The most frequent error involves fitting a 6-spline yoke to a 21-spline 1000 RPM tractor output, or a 1-3/8 in. yoke to a 1-3/4 in. output. In some cases the shaft can be physically forced into partial engagement — enough to transmit torque at low loads but with contact only at a fraction of the spline tooth depth. This partial engagement concentrates the drive load on a small number of spline tooth faces rather than distributing it across the full spline set.
The consequence is accelerated fretting wear on both the shaft yoke bore and the tractor PTO output stub. Fretting wear generates fine iron oxide debris — visually similar to rust — inside the spline engagement zone. This debris acts as a grinding compound during each rotation cycle, progressively removing material from both the yoke and the stub. After a season of operation with a partial spline engagement, the tractor PTO stub may be worn beyond the tolerance for a correctly fitting yoke — meaning the underlying tractor component now requires replacement, not just the round baler PTO shaft. The cost consequence of a mismatched spline therefore extends well beyond the driveshaft itself.
Specification Errors and Their Downstream Cost Consequences
The following table maps each common round baler PTO shaft specification error to its immediate mechanical consequence, the component most likely to fail as a result, and the approximate repair scope that follows. These are not worst-case scenarios — they reflect the typical outcome observed across the baler platforms most commonly affected by these errors.
| Specification Error | Immediate Mechanical Effect | Component at Risk | Repair Scope |
|---|---|---|---|
| Series too low (e.g. Series 4 on Series 6 application) | Repeated sub-failure overloads on U-joint cross | U-joint cross, yoke ears | Full shaft assembly replacement |
| Shaft collapsed too short | Tube impact at headland turns; yoke bore damage | Inner tube end, yoke bore, implement tongue | Shaft replacement; possible tongue repair |
| Shaft extended too long | Insufficient tube overlap; torsional fretting wear | Inner/outer tube spline profiles | Shaft replacement |
| Mismatched spline (partial engagement) | Concentrated tooth face loading; fretting debris | Shaft yoke bore, tractor PTO stub | Shaft replacement + tractor PTO stub repair |
| No CV head (standard joint at high angle) | Cyclic velocity variation at gearbox input | Baler gearbox input bearing | Gearbox input bearing replacement |
| 540 RPM shaft on 1000 RPM baler | Torque load doubled for equivalent power | U-joint cross, telescoping tubes | Premature full shaft replacement |
Manufacturing Construction: Why Series Classification Is Not Interchangeable
The physical differences between a Series 4 and a Series 6 round baler PTO shaft are not limited to the tube outer diameter. Every load-bearing dimension in the assembly scales with the series number: the U-joint cross trunnion diameter, the bearing cup bore, the yoke ear thickness, the tube wall section, and the spline profile depth all increase from Series 4 to Series 6. This means a Series 4 cross cannot be retrofitted into a Series 6 yoke, and a Series 6 guard assembly does not fit over a Series 4 tube — the series defines a complete, dimensionally coordinated assembly, not just a single component.
The telescoping tube cross-section profiles — lemon or star shapes used in agricultural series — are also series-specific. A lemon profile sized for Series 4 has a smaller minor axis diameter than the Series 6 equivalent, giving it less contact area per unit length in the sliding zone. Under the same applied torque, the contact pressure on the tube profiles is therefore higher in the Series 4 shaft — which is why fretting wear and corrosion-accelerated binding develop faster on an undersized shaft running above its rated torque, even if the shaft is otherwise correctly maintained.
Material System: How Substandard Components Accelerate the Hidden Cost
| Component | Correct Specification | Common Substandard Alternative | Consequence of Substandard Material |
|---|---|---|---|
| U-joint cross | 20CrMnTi carburised, 58–62 HRC case | Plain carbon steel, through-hardened | Brittle fracture under overload peaks; no fatigue ductility |
| Bearing cups | 52100 bearing steel, precision ground | Lower-grade steel, inadequate surface finish | Early spalling, accelerated needle roller wear |
| Telescoping tubes | Q345 cold-drawn, galvanised or epoxy-coated | Uncoated mild steel | Surface rust, binding under articulation, fretting debris generation |
| Yokes | SAE 1045 forged, normalised | Cast iron or low-grade cast steel | Ear cracking under shock loads, yoke bore distortion |
| Guard tube | UV-stabilised HDPE | Standard HDPE without UV stabiliser | Embrittlement within one season, crop fire risk from guard contact |
The material table above illustrates that a shaft can fail the specification on multiple axes simultaneously — wrong series and substandard cross material, for example — and that each axis compounds the damage independently. An operator who purchases a generic replacement round baler PTO shaft without verifying either the series rating or the cross material spec is accepting both risks at once.
Correctly Specified: EP Round Baler PTO Shaft for CASE IH Models
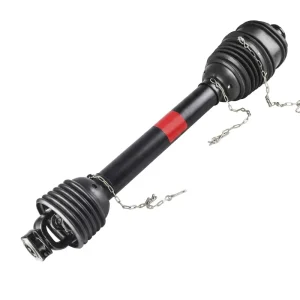
EP Round Baler PTO Shaft for CASE IH Models
A model-matched round baler PTO shaft replacement for CASE IH round baler platforms, built to the correct series, spline, and length specifications for each model designation rather than as a generic fit. The U-joint crosses are manufactured from 20CrMnTi carburised steel with 52100 bearing cup sets, eliminating the material-related failure risks that affect generic replacements. The telescoping tubes are Q345 cold-drawn with corrosion-resistant coating; yokes are SAE 1045 forged. The slip clutch is factory-assembled within the CASE IH specified release torque range. The HDPE guard assembly is UV-stabilised and CE certified. Suitable for CASE IH baler operations across North America, Western Europe, and Australasia.
Omitting the CV Head: A Cost That Lands in the Baler Gearbox
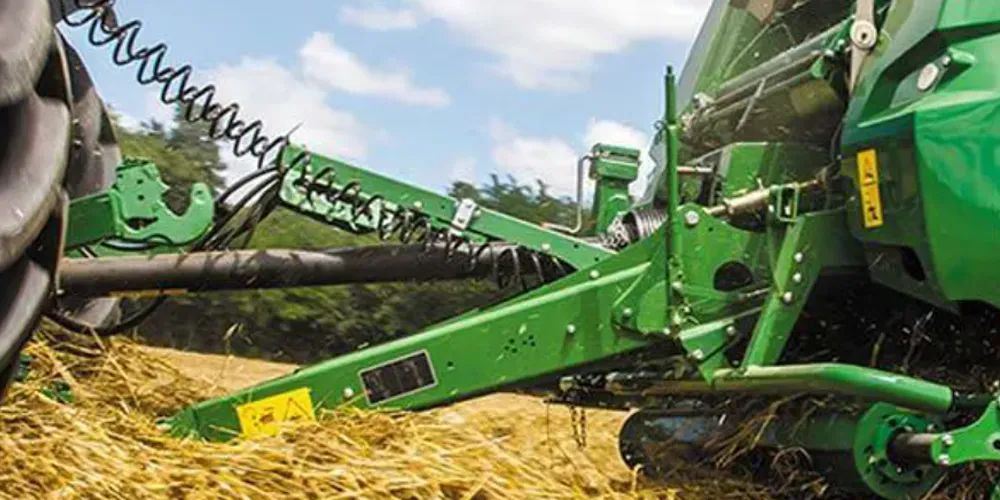
Most current-generation high-output round balers — including John Deere 9-Series and CASE IH large round baler platforms — specify a constant-velocity (CV) joint head at the front of the driveshaft, between the tractor PTO stub and the telescoping tube assembly. The CV head maintains a constant output velocity regardless of the articulation angle between tractor and baler. A standard U-joint operating at any angle above approximately 5° introduces a cyclic velocity fluctuation — two speed peaks and two troughs per shaft revolution — at the baler gearbox input.
When a standard-joint replacement shaft is fitted in place of a CV-headed original on a baler that specifies CV, this cyclic fluctuation is transmitted directly to the gearbox input shaft. The input bearing absorbs a speed variation that it was not designed to handle continuously. The effect is similar to driving with a slightly bent crankshaft — the bearing carries an alternating lateral load with each revolution rather than a pure radial load. After a season of this loading, the bearing cage develops fatigue cracks and eventually fractures, causing the input shaft to develop play and the gearbox gear mesh to become uneven. This damage is entirely attributable to the absent CV head, and it shows up as a gearbox repair bill rather than a shaft replacement — which is why the connection to the original specification error is often missed by the operator.
The Full Operational Cost Chain of a Wrong Shaft
The direct component cost of a replacement round baler PTO shaft is only the starting point of the actual expenditure when the wrong shaft is used. The full cost chain includes the repair costs for secondary components damaged by the specification mismatch, the lost revenue from downtime during the repair period, and in some cases the cost of harvested crop lost or degraded because the baling window was missed. This chain is not hypothetical — it plays out every season across farms globally that make shaft selection decisions based on availability or price alone rather than specification.
Direct Shaft Cost
The wrong shaft itself — purchased at a lower cost than the correct specification. This saving is the visible benefit that drives the original decision and the only part of the cost chain that is known at purchase time.
Secondary Component Damage
Baler gearbox input bearing, yoke bores on the tractor PTO stub, implement tongue or drawbar hardware, and in extreme cases the baler rotor or feeder gearbox. Each of these is an order of magnitude more expensive than the shaft that caused the damage.
Field Downtime
Shaft failure during harvest. Sourcing the correct replacement shaft, arranging delivery or collection, and completing the repair typically consumes one to three working days. In a tight hay weather window, this represents either crop left unprocessed or crop that deteriorates in the swath while the baler is inactive.
Repeated Replacement Cycles
An undersized shaft replaced with the same undersized shaft fails again at the same point in the following season. Operators who replace like-for-like on a prematurely failed shaft without investigating the root cause often purchase three or four incorrect shafts before the total expenditure exceeds what a single correctly specified shaft would have cost at the outset.
System-Level Components: Getting the Full Driveline Right
Selecting the correct round baler PTO shaft eliminates the shaft-level hidden costs outlined above. Selecting the adjacent driveline components to the same specification standard eliminates the system-level risks that arise when the shaft is correct but the gearbox or tractor-side adapter is not. A one-source driveline supply approach — shaft, gearbox, and universal components from a coordinated engineering range — removes the compatibility variables that generate hidden costs at the system level.
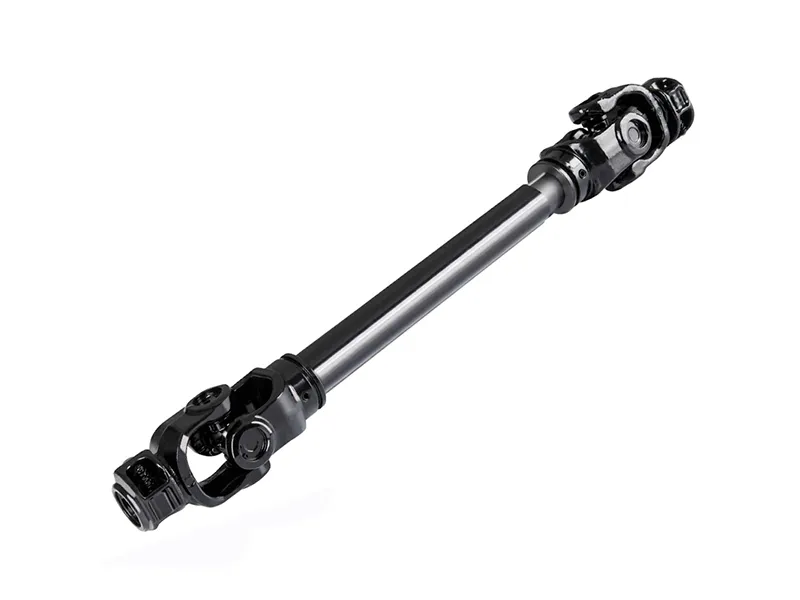
For operations running mixed baler fleets or managing tractor changes mid-season, a universal PTO driveshaft in the correct series and length provides a correctly rated alternative without the extended lead time sometimes associated with model-specific OEM shaft procurement. All series cross kits, guard components, and slip clutch disc sets are interchangeable within the series group, giving the parts inventory flexibility without sacrificing the torque rating integrity that prevents the hidden cost chain described above.
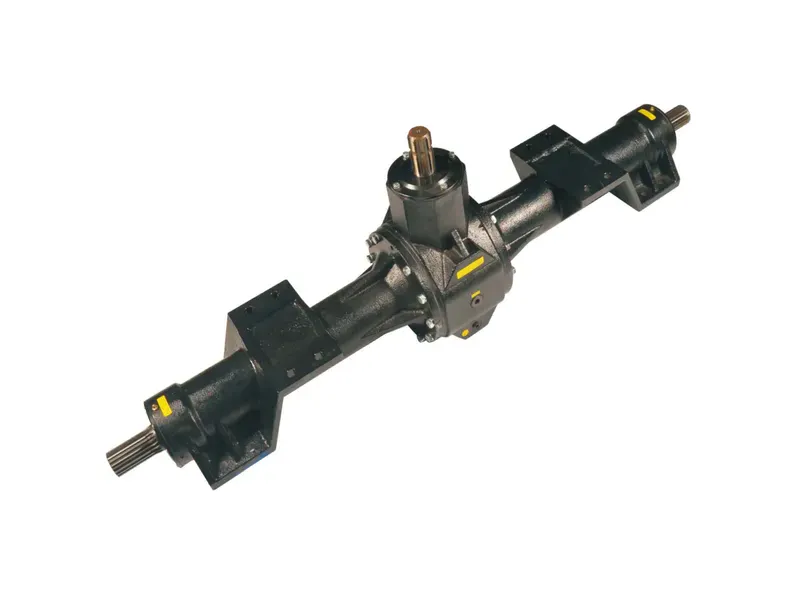
When a round baler PTO shaft specification error has already reached the gearbox — most commonly via the input bearing damage mechanism described in the CV head section above — the gearbox itself requires inspection and likely replacement before a new correctly specified shaft is fitted. Replacing the shaft without addressing the gearbox damage means the new shaft is now operating against a worn input bearing, which generates renewed vibration and accelerated shaft wear from the implement end regardless of how well the shaft itself is specified.
About the Manufacturer
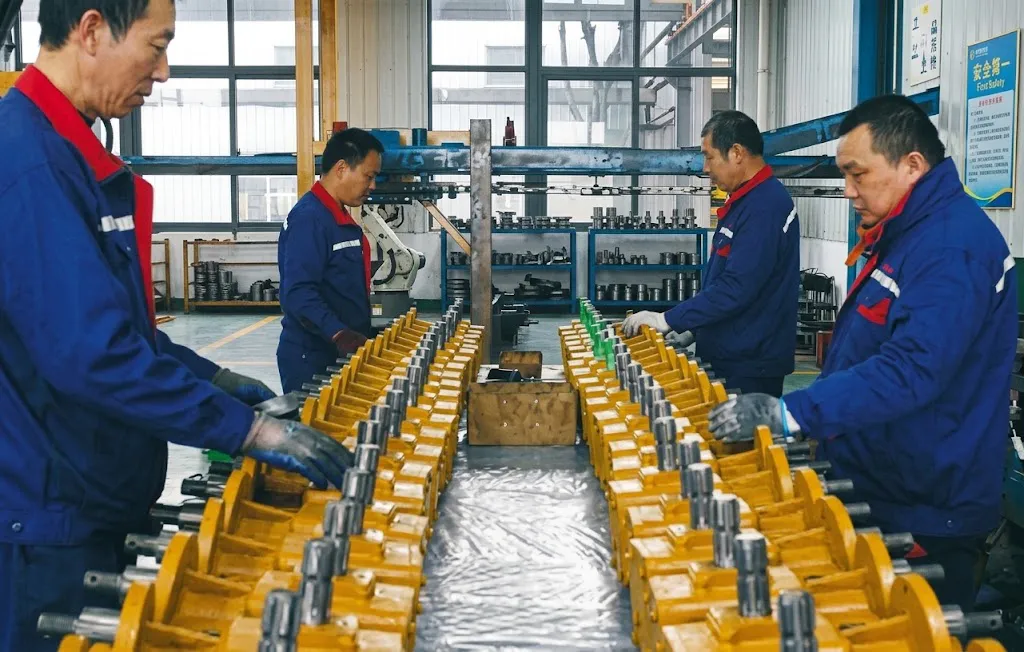
The production range covers agricultural gearboxes, worm gear reducers, planetary gear drives, power take-off shafts, hydraulic cylinders, gears, chains, and motors — manufactured under ISO 9001:2015 certification across all production stages including raw material inspection, CNC machining, assembly, and final load testing. Gearbox housings and mechanical assemblies are available in ductile iron, cast iron, cast steel, precision cast steel, and cast aluminium, with material grade selected to match each application’s structural, thermal, and weight requirements. Beyond the standard range, the engineering team produces non-standard and custom components — sprockets, worm gears, precision shafts, pulleys, and complete assemblies — to customer drawings or application descriptions, with written technical quotation provided within 24 hours of a technical inquiry or component photograph.
Workshop
Frequently Asked Questions
Editor: PXY