FAULT DIAGNOSIS GUIDE
A mechanical root-cause analysis of repeated shear bolt failure on round baler PTO shafts — covering why bolts break under normal baling loads, the driveline and operational factors behind each cause, and when upgrading to a friction slip clutch resolves the problem permanently.
A shear bolt that breaks during a blockage event is doing its job. A shear bolt that breaks repeatedly during normal baling — in an even windrow, at steady ground speed, with no obvious obstruction — is telling the operator that something in the driveline or operating setup is generating torque spikes above the bolt’s rated shear load during conditions that should not be producing them. Replacing the bolt and resuming baling without investigating the cause produces the same result within minutes to hours. The bolt is not the problem; it is the symptom.
This guide works through the five most common root causes of repeated shear bolt failure on round baler PTO shafts, the mechanical evidence that distinguishes each cause, and the corrective action — ranging from a simple bolt specification check to a full upgrade from shear bolt protection to a friction slip clutch assembly. The round baler platforms most commonly affected include New Holland 630, New Holland 648, older CASE IH fixed-chamber models, and smaller John Deere balers operating at 540 RPM — all of which shipped with shear bolt protection rather than friction clutch as standard.
How a Shear Bolt Works on a Round Baler PTO Shaft
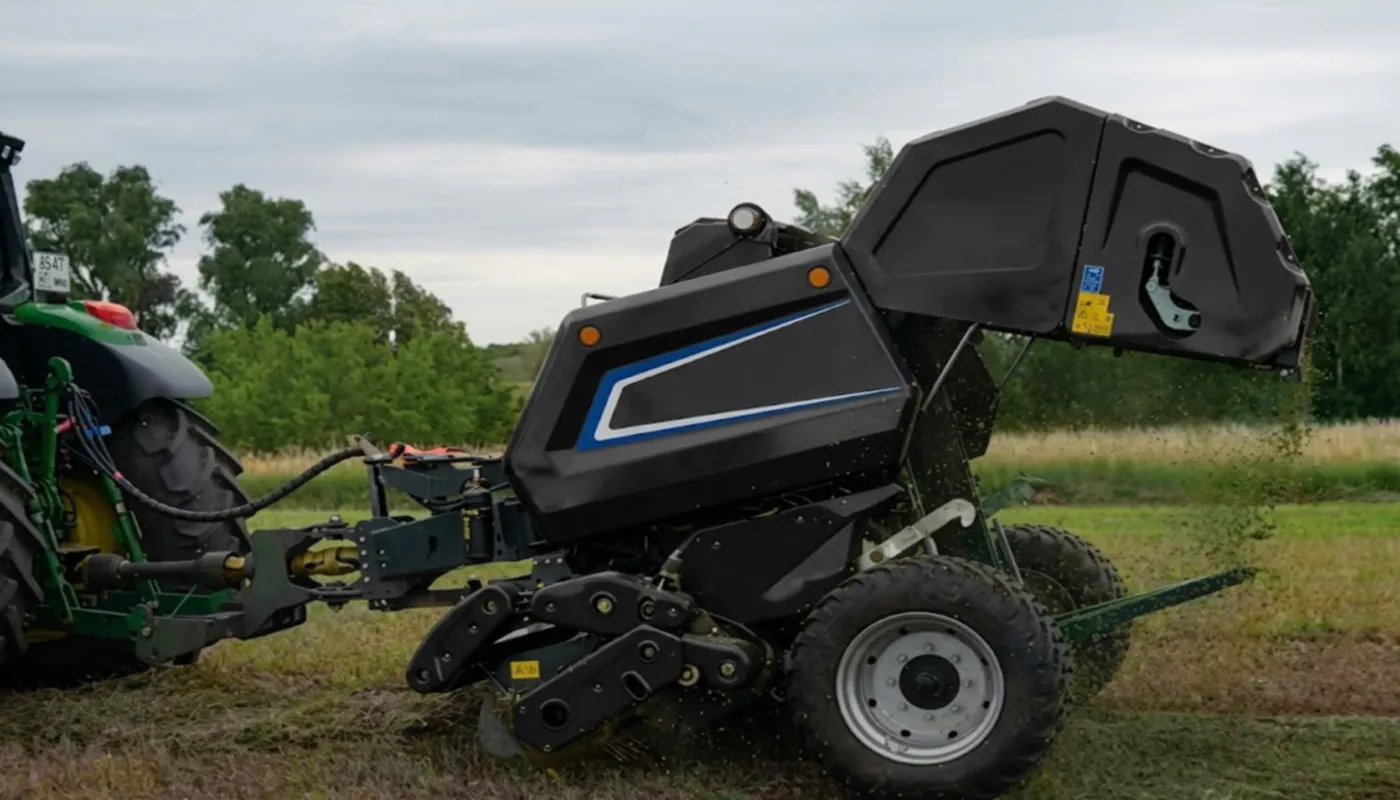
A shear bolt on a round baler PTO shaft is a deliberate weak point installed in the driveline to protect the baler gearbox from damage when the baler rotor or pickup encounters an obstruction that would otherwise stall the drive. The bolt passes through a cross-drilled hole in the yoke and the splined connection between the yoke and the PTO shaft stub, holding the two components in driving engagement. When the torque transmitted through the connection exceeds the bolt’s cross-sectional shear strength, the bolt fractures cleanly — disconnecting the drive and preventing the torque peak from reaching the gearbox. Recovery requires the operator to stop the tractor, exit the cab, remove the broken bolt halves, and insert a new bolt of the correct specification before baling can resume.
The shear bolt works correctly in this scenario — one fracture per genuine blockage event, clean break, quick replacement, and the gearbox is protected. The problem emerges when the fracture frequency rises above one per real blockage event. If bolts are breaking in normal crop conditions without any obvious jammed material, the shear bolt is being called on to absorb loads that the driveline system should not be generating under those conditions. The root cause is never the bolt itself — it is one of the operating or driveline factors described in the sections below.
Root Cause 1: Wrong Bolt Grade or Diameter
The most common cause of repeated shear bolt failure is the use of a bolt with the wrong shear rating — most often a bolt that is too soft, too small in diameter, or cut from generic hardware stock rather than the specific grade specified in the baler operator’s manual. Shear bolts are manufactured from a specific steel grade and to a specific diameter so that they fail at a defined torque threshold. A bolt sourced from a general hardware supplier in the correct thread size but a different material grade may shear at 40–60% of the intended torque — meaning it fractures under normal baling load rather than during an overload event.
The baler’s operator’s manual specifies the exact bolt grade, diameter, thread pitch, and quantity. This specification is not interchangeable with the nearest available fastener; the shear cross-section area and material strength together define the release torque, and changing either variable shifts the release point. Grade 8.8 and Grade 10.9 bolts of the same diameter have very different shear strengths — a Grade 8.8 bolt in a position specified for Grade 10.9 will fail repeatedly in normal baling. Before investigating any other cause, confirm the bolt specification against the baler manual and replace with the exactly specified item.
Root Cause Analysis: Five Causes and Their Diagnostic Evidence
| Root Cause | Diagnostic Evidence | When It Breaks | Corrective Action |
|---|---|---|---|
| Wrong bolt grade/size | Clean shear face; bolt diameter or markings do not match manual spec | During light to normal baling load | Source exact bolt specification from baler parts manual; never substitute generic hardware |
| Incorrect PTO speed | Tractor running at 540 RPM on a 1000 RPM baler, or vice versa; high torque load relative to power | Immediately at PTO engagement or during heavy windrow pass | Confirm tractor output speed matches baler specification; adjust tractor PTO gear selection |
| Excessive operating angle | Bolts break more frequently on headland turns or when tractor turns sharply mid-field | During turns; immediately on engagement after a tight turn | Check hitch geometry; reduce maximum turn angle; confirm shaft is not fully collapsed at turn |
| Sticky baler rotor startup | Bolts break at PTO engagement, not during baling; crop residue inside baler mechanism at startup | At engagement; first 2–3 seconds after PTO is switched on | Clear any crop from rotor before engaging PTO; engage at low engine revs and increase gradually |
| Shaft series under-specification | Bolts break at same point in each baling cycle; shaft series rating lower than baler requires | During peak bale compression; consistent timing across multiple events | Verify shaft series against baler spec; replace with correct series; upgrade to friction slip clutch |
Manufacturing Construction: Shear Bolt Yoke Design and Its Limitations
The shear bolt connection is a designed-in limitation of the yoke rather than a separately added component. The yoke is machined with a transverse bore through the collar that engages the PTO stub; the bolt passes through this bore and seats against a corresponding groove or cross-hole in the stub. The shear plane — the point at which the bolt is intended to fracture — sits at the interface between the yoke bore and the stub surface. This geometry means the bolt fails in double shear, with two shear planes acting simultaneously, which gives more consistent fracture torque than a single-shear configuration.
The limitation of this design relative to a friction slip clutch is that recovery from each fracture event requires manual intervention — stopping the tractor, exiting the cab, removing the bolt halves from the bore with a punch or screwdriver, and installing a replacement bolt with the correct torque applied to the retention nut where one is used. In conditions where blockage frequency is high — dense first-cut grass, wet silage material, crop with embedded stones in New Zealand paddocks or eastern European fields — this manual recovery cycle becomes the primary constraint on baling productivity. Each bolt replacement event costs four to eight minutes; across a shift with ten blockage events, that is up to an hour of lost baling time per machine per day.
Root Cause 2: PTO Speed Mismatch Between Tractor and Baler
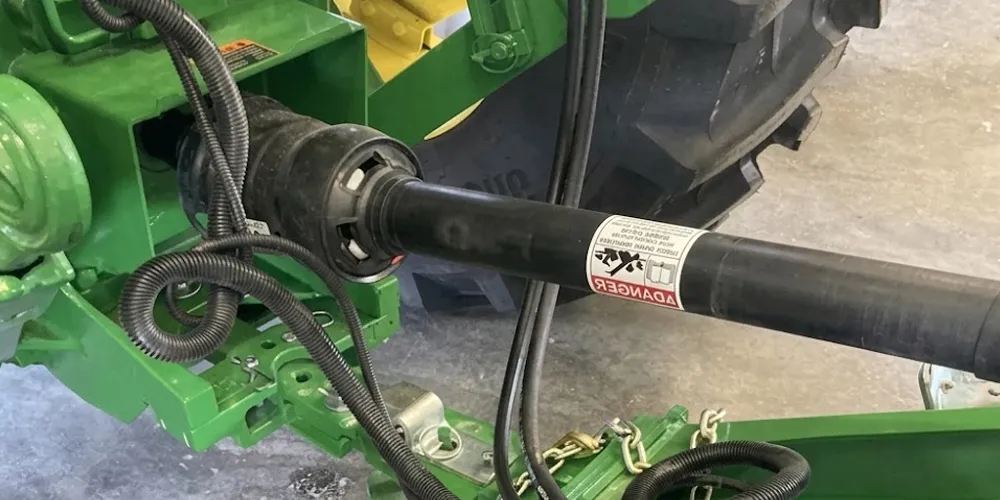
Running a baler at the wrong PTO speed is one of the fastest ways to produce repeated shear bolt failure. The relationship between power, speed, and torque means that a baler designed to receive its rated power at 1000 RPM will receive that same power at nearly twice the torque if driven at 540 RPM from a tractor with a 540 RPM output. The shear bolt — sized for the 1000 RPM torque level — instantly exceeds its shear rating at 540 RPM even before the pickup rotor has engaged the first windrow. The reverse error — driving a 540 RPM baler at 1000 RPM — overspins the baler gearbox internal components, producing heat and vibration that the gearbox was not designed to handle at the elevated input speed.
This error occurs most frequently when an operator changes tractors without confirming the PTO speed of the replacement tractor. A tractor with a dual-speed PTO — offering both 540 and 1000 RPM from the same stub — can be switched between speeds by the operator; if the setting is inadvertently changed or not verified before connecting the baler, repeated bolt failure will occur in the first pass. The fix is straightforward: confirm the tractor PTO speed setting against the baler’s round baler PTO speed specification before engagement. On tractors with electronic PTO controls, the speed selection may be stored in a setup menu rather than a visible lever position — operators should verify the displayed RPM rather than assuming the setting from a previous session.
Material System: What the Bolt Fracture Surface Reveals
Examining the fracture surface of a broken shear bolt provides diagnostic information that points toward the root cause. A clean, flat fracture face with no deformation at the shear plane indicates the bolt fractured in a single sharp overload event — consistent with a genuine blockage or an engagement event against a stationary rotor. A fracture face that shows fibrous deformation and necking at the shear plane indicates the bolt yielded progressively under sustained torque before fracturing — consistent with an incorrect bolt grade (too soft for the application) or a sustained overload condition such as a PTO speed mismatch.
| Fracture Surface Appearance | Likely Root Cause | Next Diagnostic Step |
|---|---|---|
| Clean flat shear with no deformation | Single sharp overload — genuine blockage or engagement spike | Check for crop in baler at each engagement; confirm rotor is clear before PTO engagement |
| Fibrous or necked fracture — bolt stretched before breaking | Wrong bolt grade (too soft); sustained torque overload | Verify bolt grade against manual; check PTO speed setting |
| Multiple fracture events visible (staged cracks) | Fatigue fracture from repeated sub-failure torque cycles | Shaft series likely under-rated for the peak torque being generated |
| Shear offset at fracture (not perpendicular to bolt axis) | Yoke bore or stub cross-hole worn or out of alignment | Inspect yoke bore and stub cross-hole for wear; replace yoke if bore is enlarged |
Root Cause 3: Operating Angle and Engagement Shock
Excessive Operating Angle
A round baler PTO shaft operating above its rated maximum articulation angle transmits a velocity fluctuation through the yoke connection during each shaft revolution. This fluctuation imposes a cyclic torque variation on the bolt — peaks above the mean torque and troughs below it — at a frequency of twice per shaft revolution. At 540 RPM, this means 1,080 torque peaks per minute at the shear bolt. If the peak-to-mean ratio at the operating angle is large enough to push the peak torque above the bolt’s shear threshold, the bolt will fracture at the first or second peak after engagement. The diagnostic sign is that bolts break more frequently during turns or at headland angles, where the articulation is greatest.
Engagement Shock
Engaging the PTO at full engine revs against a stationary baler rotor — particularly after clearing a blockage or at the start of a new pass — generates a torque spike at the shear bolt that is several times larger than the steady-state baling torque. The rotor’s inertia resists acceleration; the full engine torque arrives at the shear bolt before the rotor has reached operating speed, concentrating the entire acceleration load on the bolt in a fraction of a second. On shear-bolt equipped round baler PTO shafts, the correct engagement procedure is to reduce engine revs to near idle, engage the PTO lever, and then increase revs gradually until the baler reaches operating speed. This soft-start approach distributes the acceleration torque over several seconds rather than milliseconds, keeping the peak bolt load below the shear threshold.
The Permanent Solution: Upgrading to a Friction Slip Clutch Round Baler PTO Shaft
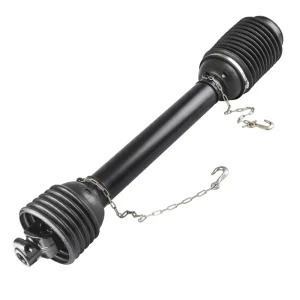
EP Round Baler PTO Shaft — John Deere 469 / 569 Series with Friction Slip Clutch
For operators who have resolved the root cause of repeated shear bolt failure and now want to eliminate the manual recovery cycle permanently, a round baler PTO shaft equipped with a friction slip clutch is the replacement of choice. The 80° wide-angle friction slip clutch on this John Deere 469 / 569 fit releases automatically at the calibrated overload torque — without bolt replacement — and re-engages immediately once the blockage clears. Built on Series 6 with 20CrMnTi carburised crosses and precision-ground 52100 bearing cups, with front yoke compatibility for 1-3/8 in. × 6 and 1-3/8 in. × 21 spline 1000 RPM tractor outputs. CE-certified guard assembly. The transition from shear bolt to friction clutch on a John Deere round baler PTO shaft is one of the highest-ROI maintenance upgrades available on older baler platforms that shipped with bolt protection as standard.
Shear Bolt vs Friction Slip Clutch: A Practical Comparison for Round Baler Operators
| Attribute | Shear Bolt | Friction Slip Clutch |
|---|---|---|
| Recovery after blockage | Manual — exit cab, remove bolt halves, insert new bolt | Automatic — clutch re-engages when blockage clears |
| Time lost per blockage event | 4–8 minutes minimum | Under 30 seconds (clear obstruction and resume) |
| Torque release consistency | Consistent per bolt grade and diameter | Adjustable within manufacturer’s specified range |
| Risk of mismatched replacement | High — incorrect bolt grade common in field supply | Low — clutch setting adjusted with tools, not substituted |
| Maintenance requirement | Carry spare bolts; replace after each fracture | Check disc condition and spring preload every 40–50 hours |
| Best suited for | Low-utilisation operations where blockages are infrequent | Higher-utilisation and contractor operations; dense or silage crops |
The Correct Diagnostic Sequence Before Replacing the Round Baler PTO Shaft
Before replacing the round baler PTO shaft or upgrading from shear bolt to friction clutch, the root cause of the repeated fractures must be confirmed — otherwise the same condition may produce the same symptom on a new shaft. The following sequence addresses causes in order of ease and probability, moving from the simplest checks to the more involved driveline assessments.
Step 1 — Confirm bolt specification
Check the broken bolt’s diameter and any visible grade marking against the baler manual. If the bolt cannot be confirmed as the correct grade and diameter, source the correct specification before proceeding to any further investigation.
Step 2 — Confirm tractor PTO speed
With the tractor stationary and PTO disengaged, confirm the selected PTO speed matches the baler’s round baler PTO speed specification. On dual-speed PTO tractors, verify the speed setting is at the value required by the baler, not the previous implement.
Step 3 — Check baler rotor for residue
With the PTO disengaged and the engine off, check the baler pickup rotor by hand for crop wrapped around the rotor shaft, stones lodged between the rotor tines, or debris blocking the rotor entry. Clear anything found before the next engagement attempt.
Step 4 — Check shaft operating angle
With the tractor at the tightest headland turn angle used in the field, observe whether the shaft is near or at its maximum articulation limit. If the shaft collapses to near its minimum or extends near its maximum, the hitch geometry needs adjustment before any shaft replacement.
Step 5 — Verify shaft series specification
If the bolt grade is confirmed correct and the PTO speed is correctly set, and bolts still break in normal baling, confirm the shaft series against the baler manufacturer’s specification. If the shaft is one series lower than specified, replace with the correct series and consider upgrading to friction clutch at the same time.
Adjacent Components to Inspect After Repeated Shear Bolt Events
Repeated shear bolt fractures — particularly those caused by PTO speed mismatch or shaft under-specification — expose the baler gearbox and the implement-end yoke to torque peaks that the round baler PTO shaft was absorbing on behalf of the gearbox. When the root cause investigation points to one of these conditions, the gearbox input and yoke bore should be inspected before a replacement shaft is installed.
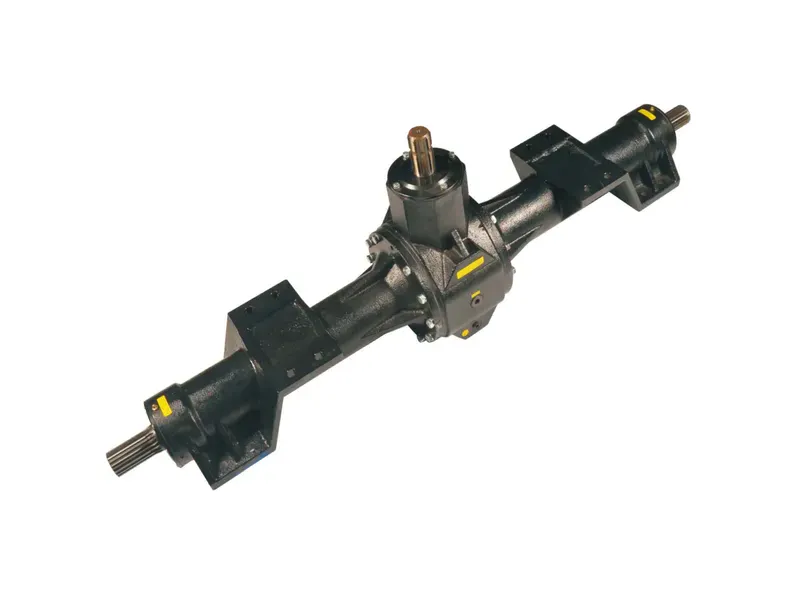
The baler gearbox is exposed to the same torque peaks that fracture the shear bolt — the bolt fractures first, but the gearbox input shaft, input bearing, and first-stage gear mesh absorb the acceleration shock energy in the milliseconds before the bolt separates. In a repeated shear bolt scenario with ten or more fracture events in a season, the gearbox input bearing should be inspected for play and the input shaft for runout. An input bearing that was damaged in this way will apply a cyclic side load to the new round baler PTO shaft immediately from installation, shortening the service life of the replacement and potentially producing the same shear pattern on a now-correctly-specified bolt.
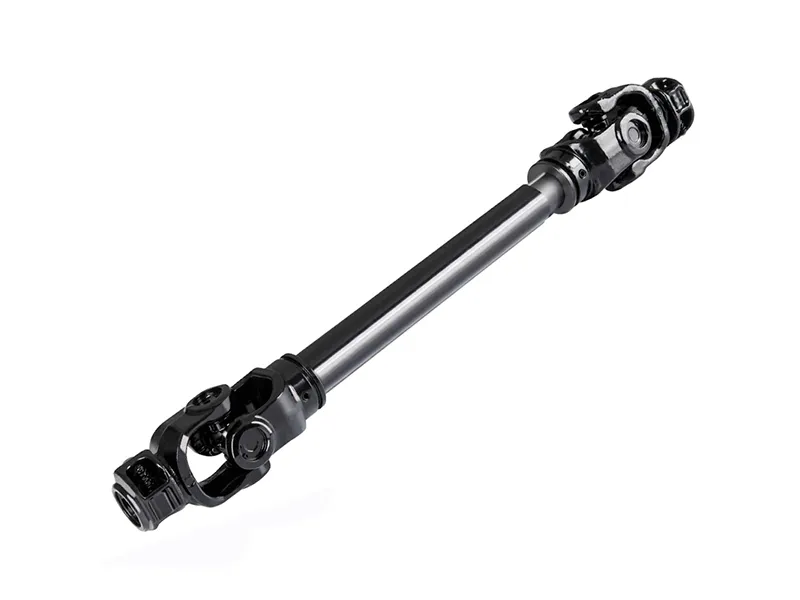
Albero di trasmissione PTO universale
When a shear bolt investigation confirms that the shaft series is correctly specified and the PTO speed is correct, but the frequency of blockage events in the crop type or field conditions being worked makes the manual recovery cycle unacceptable, upgrading to a universal PTO driveshaft fitted with a friction slip clutch is the most direct solution. A universal shaft in the correct series covers the baler’s input specification while adding self-resetting overload protection that eliminates the bolt replacement cycle entirely. Cross kits, guard assemblies, and friction disc sets are interchangeable within the same series group, simplifying the spare parts inventory for the upgraded shaft.
Informazioni sul produttore
The product portfolio covers agricultural gearboxes, worm gear reducers, planetary gear drives, power take-off shafts, hydraulic cylinders, gears, chains, and motors — all produced under ISO 9001:2015 quality certification applied from incoming material inspection through final assembly and load testing. Housing and structural assemblies are available in ductile iron, cast iron, cast steel, precision cast steel, and cast aluminium, selected by application load and operating environment. Custom and non-standard components — sprockets, worm gears, precision shafts, pulleys, and complete mechanical assemblies — are produced to customer drawings or application descriptions with written quotation returned within 24 hours.
Domande frequenti
Redattore: PXY