GENERAL BUYER GUIDE & COMPARISON
A reduktor jednobiegowy is built to run for thousands of hours between service intervals — but no mechanical system is immune to progressive wear. Recognizing the five most reliable failure indicators early is the difference between a planned maintenance stop and an unscheduled production shutdown that cascades into far greater cost.
Why Failure Recognition Matters in a Single Speed Reducer
In a reduktor jednobiegowy using worm gear architecture, the sliding contact between the hardened steel worm shaft and the bronze worm wheel generates heat and micro-surface fatigue with every revolution. When lubrication degrades, alignment shifts, or an overload event occurs, that progression accelerates. The early stages of deterioration produce measurable symptoms — thermal anomalies, oil contamination, vibration changes, seal leakage — that a trained maintenance team can act on before damage becomes severe.
Unplanned failures of a reduktor jednobiegowy in industrial facilities across the USA, UK, Australia, and Canada carry costs well beyond the gearbox unit itself: production downtime, expedited freight, and potential damage to connected equipment. Maintenance engineering studies consistently show that identifying failure precursors reduces total repair cost by a factor of three to five compared to responding after a catastrophic failure event. The five warning signs below cover the most common failure pathways in worm gear single speed reducers and apply directly to WP series units in service worldwide.
The 5 Warning Signs — At a Glance
Each of the five failure indicators below corresponds to a specific physical deterioration mechanism inside the reduktor jednobiegowy. They are listed roughly in order from early-stage to late-stage, though in practice more than one can appear simultaneously if a root cause such as chronic lubrication neglect has been active for a prolonged period.
1. Rising Operating Temperature
Under normal operation, a reduktor jednobiegowy housing runs 20–40°C above ambient depending on frame size and load. A temperature that creeps steadily higher — without any increase in load or ambient conditions — indicates either oil degradation, low oil level, or early-stage gear wear increasing friction at the worm-wheel interface. Most mineral worm gear oils begin oxidizing at an accelerating rate above 90–95°C housing surface temperature, creating a self-reinforcing thermal cycle that rapidly worsens lubrication quality. Monthly infrared thermometer readings against a commissioning baseline provide early detection of this trend for a fraction of the cost of an unplanned gearbox replacement.
2. Contaminated or Discolored Oil
Oil drained from a reduktor prędkości przekładni ślimakowej tells a clear story about internal condition. Clean, serviceable gear oil is amber and flows freely. Darkened or black oil indicates oxidation from overheating. A grayish metallic sheen confirms bronze particles from worm wheel surface wear — the tin bronze wheel (ZCuSn10Pb1 in the WP series) is the sacrificial wear element by design, but accelerated particle generation before expected service intervals points to a root cause: low oil level, incorrect viscosity, or mechanical overload. Milky or cloudy oil indicates water ingress through a degraded shaft seal, which causes immediate lubrication failure and rapid bearing and gear damage.
3. Abnormal Noise or Vibration
A well-maintained reduktor jednobiegowy runs with a characteristic low hum and minimal vibration. Any change — a higher-frequency whine, a periodic knock, or a metallic grinding component — corresponds to a physical change inside the gearbox. Bearing spalling produces a high-frequency rumble that worsens with speed. Worm wheel tooth damage produces a rhythmic knock at the mesh frequency. A vibration meter baseline taken at commissioning, with monthly trend measurements in three axes, converts a subjective noise assessment into an objective trend. A rise of 50% or more over baseline — the ISO 10816 intervention threshold — is grounds for scheduled internal inspection of the reduktor jednobiegowy.
4. Oil Leaks at Shaft Seals
The radial lip seals at the input and output shaft exits of a reduktor jednobiegowy harden and lose sealing pressure over time, especially in units that have run hot. External oil leakage is one of the most visible and easiest failure precursors to detect during routine walkaround inspections. Beyond the mess, a leaking seal removes oil from the internal bath — oil that is no longer available for lubrication. WP series oil capacities range from 0.4 L (40-frame) to 5.2 L (large WPZ/WPKZ frames). A small-frame unit losing 0.2 L per day through a seal failure reaches critically low oil levels in two days of undetected leakage, accelerating gear and bearing wear to a degree that may require full gearbox replacement rather than just seal renewal.
5. Inconsistent Output Speed
A functioning reduktor jednobiegowy delivers a steady output shaft speed that is a fixed fraction of the motor input — for WP series units, the ratio range is 10:1 to 60:1. Irregular output shaft motion — visible as driven equipment hunting or confirmed by tachometer fluctuation — is a late-stage indicator that the mechanical connection between input and output is no longer transmitting smoothly. In a reduktor ślimakowy, this typically results from advanced worm wheel tooth spalling (where the worm partially skips over damaged tooth areas) or a slipping keyway connection at the output shaft. Unlike the earlier warning signs, output speed inconsistency means damage is already active and the unit needs immediate assessment rather than deferred investigation.
Failure Sign Reference Table
This table summarizes each warning sign, its root cause, and the appropriate maintenance response — formatted as a field reference for maintenance engineers managing a fleet of reduktor jednobiegowy units in North America, Europe, Australia, or Asia.
| Warning Sign | Root Cause | Risk if Ignored | Recommended Action | Urgency |
|---|---|---|---|---|
| Rising temperature | Oil degradation or low level | Oil oxidation cycle, gear damage | Check level, drain and refill | Medium — within one week |
| Contaminated oil | Overdue change or overload | Bronze wheel pitting, accelerated wear | Drain, inspect wheel faces | Medium — current maintenance window |
| Noise / vibration change | Bearing spalling or gear damage | Progressive internal damage | Vibration analysis, bearing check | Medium-High — within 48 hours |
| Oil leaks at seals | Lip seal hardening or wear | Low oil, seizure risk | Replace lip seals immediately | High — same day |
| Output speed irregularity | Advanced gear or bearing failure | Complete gearbox failure, connected damage | Immediate shutdown, full inspection | Critical — stop now |
Manufacturing Structure and Material System
Understanding the construction of a reduktor jednobiegowy clarifies why these failure modes occur and where to look during an internal inspection. In the WP series, the housing is produced from HT250 grey cast iron — a material chosen for its vibration damping, machinability for tight bore tolerances, and compressive strength under bearing preload. The worm shaft is machined from 20CrMnTi alloy steel, case-carburized and hardened to 58–62 HRC, then precision-ground to the final thread form. This surface hardness is what makes the worm shaft the long-life element in the gear pair.
The worm wheel in a reduktor prędkości jednostopniowy is centrifugally cast from ZCuSn10Pb1 tin bronze — intentionally softer than the hardened steel worm so that wear occurs preferentially on the wheel rather than the worm shaft. This means the worm wheel is the primary wear indicator and the expected replacement component in a correctly maintained reduktor prędkości ślimakowej. When oil analysis finds accelerated bronze particle generation or a wheel inspection reveals pitting before the expected replacement interval, the root cause is almost always a deviation from correct lubrication practice, an overload condition, or an installation error — not an inherent flaw in the material specification of the reduktor jednobiegowy.
Sourcing a Replacement or Spare Single Speed Reducer?
If a unit in your facility is showing any of the warning signs described here, the full WP series reduktor jednobiegowy range — from compact 40-frame models to large 250-frame units — is available with complete technical documentation for replacement planning.
Product Reference for Replacement Planning
Kiedy reduktor jednobiegowy failure investigation concludes that replacement is more practical than repair, having accurate frame and model data from the failed unit simplifies sourcing a dimensional replacement. The two models below are frequently specified as replacements in US and Australian facilities where the WP series is already in service.
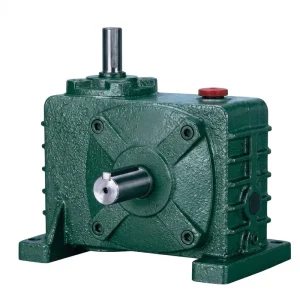
EP-WPZ — reduktor jednobiegowy o pojemności oleju od 0,4 do 5,2 l
The WPZ model covers oil capacities from 0.4 L to 5.2 L across frame sizes — data that is directly relevant to calculating how quickly a detected seal leak depletes the internal oil supply. This foot-mounted reduktor jednobiegowy has a bottom-mounted drain plug that simplifies oil drain-and-inspect procedures without removing the unit from its baseplate. It accepts input power from 0.12 kW to 15 kW with a 10:1 to 60:1 ratio range across standard frame sizes.
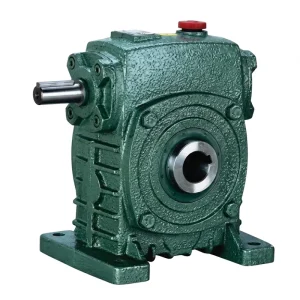
EP-WPKS — reduktor jednobiegowy od 4 do 365 kg
The WPKS series spans 4 kg to 365 kg, covering drives from light conveyor applications to heavy-duty material handling. For facilities in Australian mining or US processing operations where unplanned gearbox downtime carries significant production cost, stocking a spare WPKS unit in the appropriate frame is a practical risk management approach. The compact WP series footprint typically allows a replacement reduktor jednobiegowy to be installed within a standard maintenance shift window.
Kompatybilne komponenty układu napędowego
When replacing a failed reduktor jednobiegowy, checking and potentially replacing connected drive system components — motor and downstream gearing — alongside the gearbox prevents recurring failures caused by damage that occurred to those components during the gearbox failure event.
Silniki elektryczne
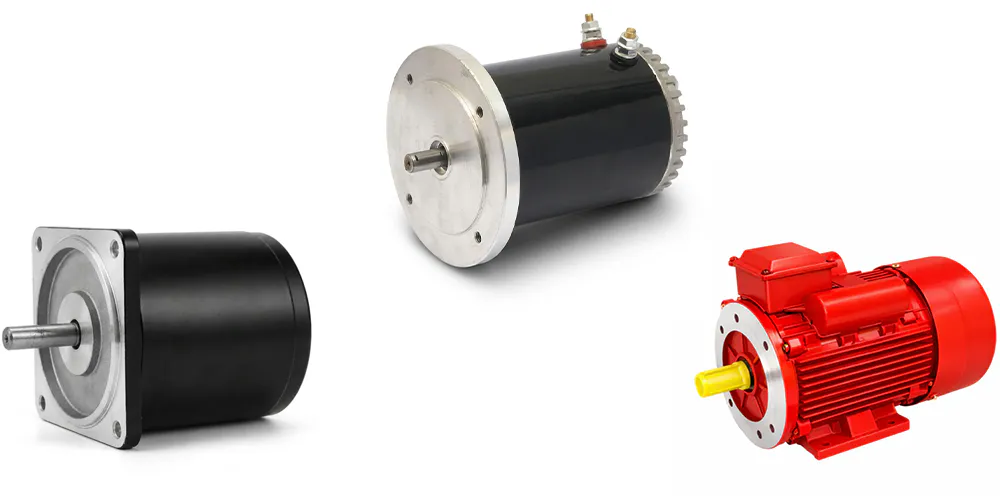
A motor that drove a deteriorating reduktor jednobiegowy through extended overload or vibration may have developed bearing wear or winding stress. Inspecting the motor — and sourcing a matched silnik elektryczny replacement if required — alongside the gearbox ensures the rebuilt drive system starts fresh on both sides of the transmission interface. The WP series reduktor jednobiegowy accepts IEC B3, B5, and B14 frame motors across the 0.12 kW to 33 kW range.
Przekładnia ślimakowa
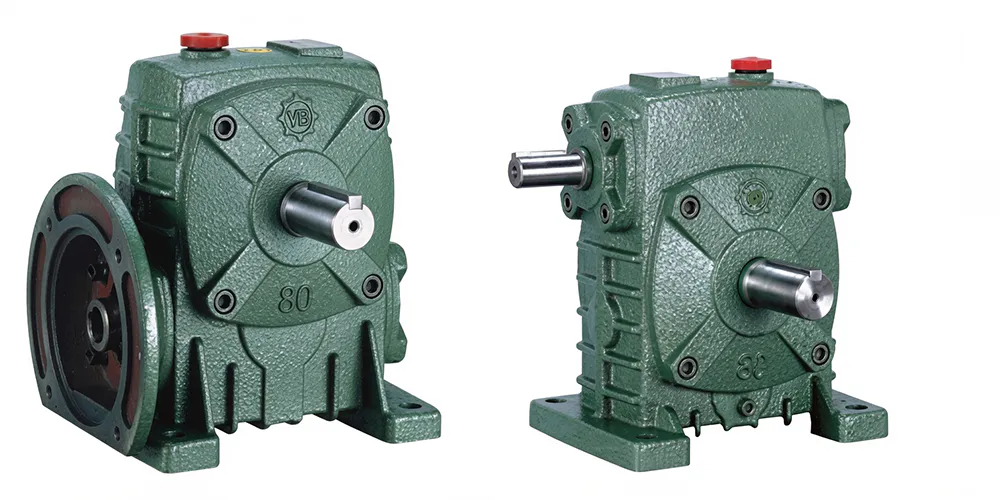
For applications where a two-stage drive ratio provides better thermal management than a single-stage unit at the same output speed, a worm gearbox from the WP double-stage series extends the ratio range to 1/900. The shared housing material specification across WP single and double-stage families simplifies interfacing, and moving to a two-stage reduktor ślimakowy can resolve chronic thermal issues in single-stage units that were originally slightly undersized for the installed duty cycle.
O zakładzie produkcyjnym
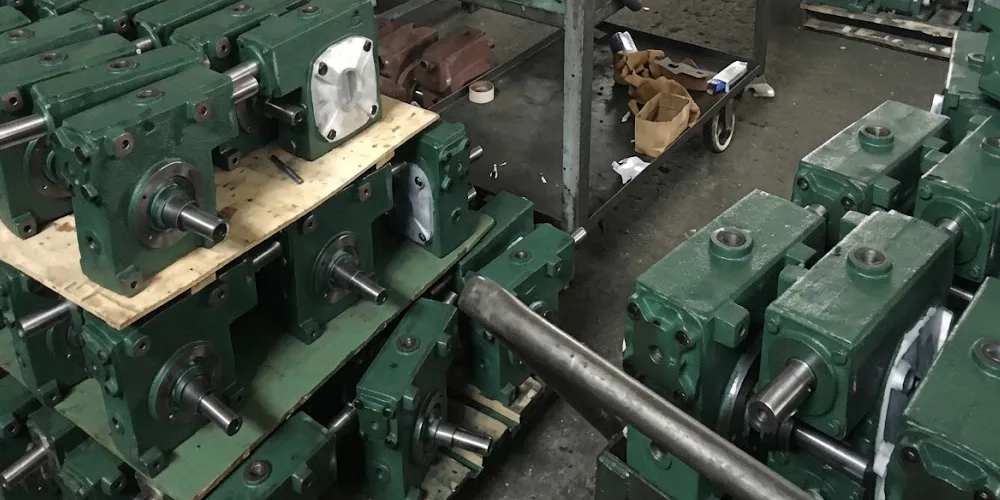
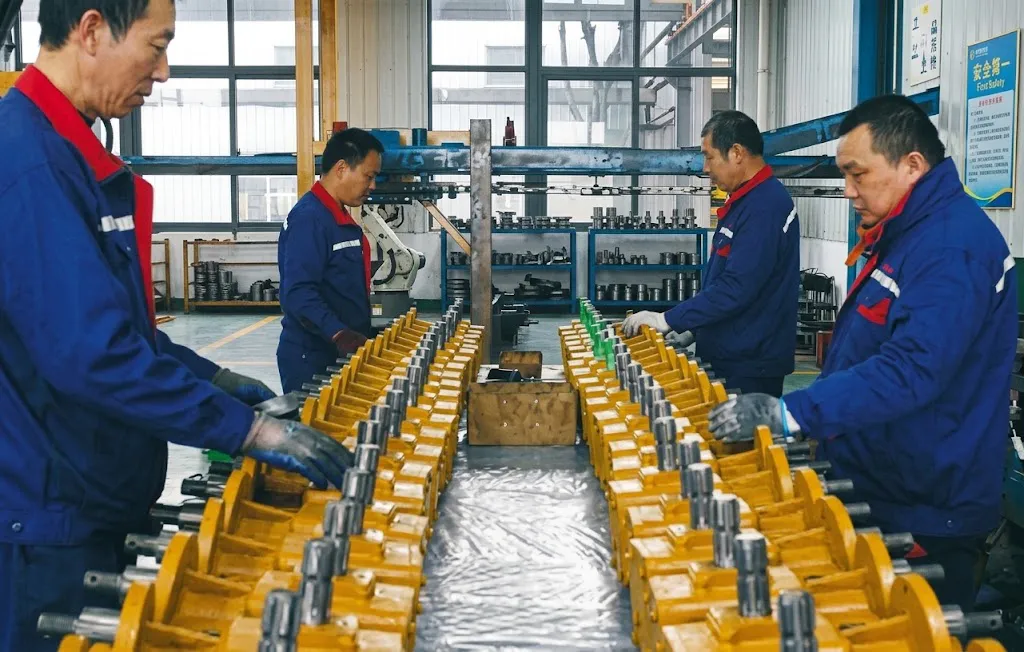
Our production facility manufactures a broad range of industrial and agricultural power transmission products — worm gear reducers, planetary gear drives, agricultural gearboxes, power take-off shafts, hydraulic cylinders, gears, sprockets, chains, and motors. The reduktor jednobiegowy series covers both foot-mounted and shaft-mounted configurations across the WP family of frame sizes. Housings are produced in ductile iron, grey cast iron, cast steel, precision cast steel, and cast aluminum. Gears, sprockets, worm gears, pulleys, worms, and shafts — both standard catalog and non-standard parts to customer drawings — are manufactured in-house under ISO 9001:2015 quality management certification.
Jako producent reduktorów jednobiegowych with production and export experience, we supply customers in the USA, UK, Australia, Canada, the Netherlands, Brazil, South Korea, Colombia, and other international markets with OEM customization, private-label supply, and technical support for maintenance planning programs. Replacement worm wheel and shaft sets, matched shaft seals, and full gearbox units are available through our export supply channel to support field maintenance programs globally.
Warsztat
Często zadawane pytania
These questions address the practical concerns that maintenance engineers raise when evaluating a reduktor jednobiegowy for condition and deciding on corrective action.
How do I know if my single speed reducer needs an oil change or a bearing replacement in a US food processing conveyor application?
Correlate two data points: oil condition and vibration level. If the oil is dark or carries fine metallic particles but vibration readings remain near baseline, lubrication degradation is the likely cause — a drain-and-refill resolves it. If the oil is clean but vibration has risen 30–50% above the commissioning baseline, a bearing issue is more probable and warrants an internal inspection of the reduktor jednobiegowy rather than another oil change. In US food processing applications where H1-rated lubricants are required, always confirm the correct food-grade oil is in use; wrong lubricant grades accelerate both thermal and mechanical degradation simultaneously.
What are the most common reasons a worm gear single speed reducer overheats during 24-hour continuous shifts in an Australian mining facility?
In Australian mining operations, the three most common overheating causes are: incorrect oil viscosity for elevated ambient temperatures (ISO VG 320 or synthetic equivalents perform better above 35°C ambient compared to standard ISO VG 220), oil fill below the correct level for the mounting orientation, and prolonged mechanical overloading above the single speed reducer’s rated output torque. Dust ingress through degraded shaft seals is also more prevalent in open pit environments and introduces abrasive contamination that accelerates gear wear and adds further heat generation. Monthly drain-and-assess oil inspections on high-duty units catch these conditions before they become failure events.
Which failure signs in a single speed gear reducer require an immediate shutdown versus a scheduled investigation in a UK packaging line?
Output speed inconsistency and metallic grinding noise should trigger an immediate or same-shift planned shutdown — these are late-stage indicators of damage that is actively progressing. Rising temperature without noise change can typically be monitored to the end of the current shift and investigated at the next scheduled window. Oil seal leakage occupies a middle ground: if the oil level is still within the acceptable range and the leak rate is slow, the reduktor jednobiegowy can complete the shift, but the seal must be replaced before the following production day. On any UK packaging line, a monitored warning sign should never remain unaddressed for more than one full production cycle once identified.
How often should vibration measurements be taken on a single stage speed reducer driving a grain elevator in a Canadian agricultural facility?
Dla reduktor prędkości jednostopniowy on a Canadian grain elevator running seasonal operations of 2,000–3,000 hours, vibration measurement at the start of each season and at the seasonal midpoint covers the main risk windows. A pre-startup check before the first motor power application each season — oil level, seal inspection, hand-rotation check for bearing roughness — catches any deterioration that occurred during off-season storage. During peak harvest when the unit runs continuously, a monthly vibration check adds confidence between the formal seasonal measurements and allows deterioration trends to be caught before they interrupt operations at the worst possible time.
Where can maintenance teams in the Netherlands or South Korea source replacement worm wheel sets for a WP series single speed reducer?
Replacement worm wheel and shaft sets for WP series reduktor jednobiegowy units in the Netherlands, South Korea, and other international markets can be ordered through our export supply channel. When ordering, provide the frame size designation, housing model (e.g., WPZ, WPKS), and the reduction ratio — these three parameters define the gear geometry and bronze specification. Matched shaft seals in the correct lip diameter for each frame can be included in the same order, so a planned worm wheel replacement and seal renewal are completed in a single maintenance event, minimizing the number of planned shutdowns required per service cycle.
Redaktor: PXY